

All Products
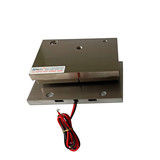
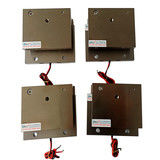
100N High Thrust Short Stroke Voice Coil Actuator for Wafer Cutting Blade Feed



| Place of Origin | Suzhou, Jiangsu, China |
|---|---|
| Brand Name | SUPT MOTION |
| Certification | ISO 9001:2015, CE |
| Model Number | VCAP0100-0020-00A |
| Minimum Order Quantity | 1 Piece |
| Price | USD 320-420 / Piece |
| Packaging Details | Cleanroom bag, ESD safe tray, shock absorbing foam, export carton with desiccant |
| Delivery Time | 5-7 working days for samples, 18-25 working days for batch orders |
| Payment Terms | T/T |
| Supply Ability | 200 Pieces per Month |
Product Details
| Model | VCAP0100-0020-00A | Axis Role | Blade Or Tool Infeed |
|---|---|---|---|
| Peak Force | 100 N | Continuous Force At 25C | 47 N |
| Total Stroke | 4 Mm | Max Voltage | 41.2 V |
| Back EMF Constant | 80.1 V/m/s | Body Size | 110 X 105 X 51 Mm |
| Force Feedback | From Coil Current | Protection | Sealed Magnet Track |
| Typical Application | Dicing Saw, Laser Scribe, Cleaving | ||
| Highlight | 100N voice coil actuator,short stroke linear actuator,wafer cutting blade feed actuator |
||
Product Description
Product Overview
The VCAP0100-0020-00A provides controlled feed for wafer dicing processes: this includes blade feed on dicing saws, feed of splitting tools, and control of scoring depth on laser stations. At 25°C, this product can generate a peak thrust of 100 N and a continuous thrust of 47 N over a stroke of 4 mm, with a maximum voltage of 41.2 V, a back-EMF constant of 80.1 V/m/s, and dimensions of 110 × 105 × 51 mm. The short stroke of the flat voice-coil motor is well-suited to the process requirements, as the cutting blade only needs to penetrate a few hundred micrometres into the material; it is precisely this short stroke that enables direct-drive feeding.
Solution
The quality of semiconductor material cutting depends primarily on the feed force and its stability, rather than the nominal feed rate. When the blade load fluctuates, silicon, glass and ceramics exhibit different chipping behaviours; however, ball screw feed cannot distinguish between its own friction and the cutting force, meaning the process must operate based on assumed values. A voice coil acts as a force source: a command of 5 N results in a force of 5 N being applied to the blade, and the current curve directly reflects the cutting load. This enables constant-force feed, cut width control and early warning of blade dulling or chipping. This characteristic also enables depth control on thin wafers—where hard stops would cause the chip to crack: the spindle advances until the programmed force is reached and then maintains that force, so that tape expansion, wafer warping and blade wear are absorbed by the closed-loop system rather than borne by the material. As the coil has no mechanical play, the repeatability of the retraction and re-advance cycles is in the micrometre range, which is crucial for step cutting and multi-pass processing on compound semiconductor wafers.

Specifications
| Parameter | Value |
|---|---|
| Model | VCAP0100-0020-00A |
| Axis role | Blade or tool infeed, force controlled cutting |
| Peak force | 100 N (intermittent) |
| Continuous force at 25°C | 47 N |
| Total stroke | 4 mm |
| Maximum voltage | 41.2 V |
| Back EMF constant | 80.1 V/m/s |
| Body size | 110 × 105 × 51 mm |
| Force feedback | From coil current, no separate load cell needed |
| Stiffness | Direct drive, no screw compliance in the loop |
| Cooling | Heat sink plate required above 35 N average force |
| Protection | Sealed magnet track for wet dicing environments |
| Mounting | Base flange, four M6 threads |
Application
Blade infeed on dicing saws, laser scribe and stealth dicing depth axes, cleaving tool advance for compound semiconductors, wafer edge trimming, glass and ceramic substrate cutting, and thin film trimming stations where a controlled contact force is critical.
FAQ
Q: How is depth controlled when the wafer is bowed?
A: Depth is reached through force rather than a hard stop: the axis advances until the programmed cutting force is achieved and then holds it, so wafer bow and tape expansion are compensated by the loop instead of loading the die.
Q: Can cutting force be logged per cut?
A: Yes. Coil current is proportional to force, so the drive can stream a force trace for every street, which is useful for blade wear trending and for detecting chipping events.
Q: Is the actuator protected against dicing coolant?
A: The magnet track is sealed for wet environments. For aggressive spray, mount the actuator behind a splash guard with only the tool holder passing through the curtain.
Q: Why only 4 mm of stroke?
A: The stroke covers blade infeed plus retract clearance and a safety margin, and a short stroke keeps the magnetic circuit compact and the force density high. Longer travel is available in the 16 mm and 20 mm models.
Recommended Products